Elevating Food Safety Standards: Mettler Toledo Unveils M50 R-Series AdvancedLine Metal Detectors
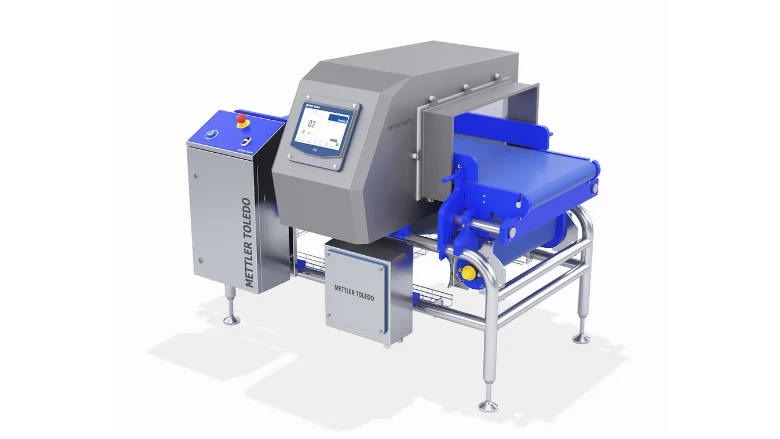
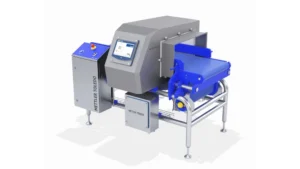
In an era where food safety regulations are becoming increasingly stringent and the margin for error in manufacturing is non-existent, the Mettler Toledo Product Inspection Group has taken a significant step forward. The company recently announced the North American launch of its M50 R-Series AdvancedLine metal detectors—a suite of high-performance inspection systems engineered to meet the dual demands of rigorous contaminant detection and seamless digital integration.
As food manufacturers navigate the complexities of global supply chains and heightened consumer expectations, the M50 R-Series arrives as a pivotal tool for those seeking to bolster their quality control protocols. By blending advanced electromagnetic technology with artificial intelligence, the series promises not only to catch smaller, more elusive contaminants but to do so with an efficiency that minimizes costly production downtime.
The Technological Leap: Precision Through Innovation
The core strength of the M50 R-Series lies in its proprietary detection architecture. Food contaminants are rarely uniform; they vary in shape, size, and composition. Detecting a spherical piece of stainless steel is fundamentally different from identifying a thin, jagged piece of wire—a common hazard in processed food environments.
The Power of eDrive PLUS
At the heart of the M50 R-Series is the eDrive PLUS technology. When paired with a 900-kilohertz (kHz) operating frequency, this system achieves a substantially higher magnetic field strength than traditional models. This increased intensity allows the detectors to achieve superior sensitivity for wire-shaped and non-spherical contaminants, which have historically been the "Achilles’ heel" of metal detection technology. By focusing on the physical orientation of these difficult-to-spot particles, Mettler Toledo has effectively raised the bar for what constitutes "clean" product lines.
AI-Driven Accuracy
One of the most persistent frustrations for food safety managers is the "false reject." Every time a metal detector incorrectly flags a safe product as contaminated, it creates a ripple effect: the product must be inspected, packaging may be damaged, and the production line must be stopped, leading to significant financial losses.
The M50 R-Series addresses this through the integration of 3S PLUS algorithms and AI-based machine learning. These systems learn the specific "signature" of a production line, distinguishing between true metallic threats and harmless product effects (such as the mineral content or moisture levels inherent in certain foods). By filtering out noise more effectively, the R-Series ensures that the equipment remains sensitive to actual risks while dramatically reducing the frequency of false alerts.
Chronology of Development and Market Entry
The development of the M50 R-Series is the culmination of years of iterative research and development by Mettler Toledo. While the official North American launch marks the latest milestone, the timeline of the product’s evolution reflects the company’s broader strategy to digitize the factory floor:
- Preliminary R&D Phase: Mettler Toledo engineers focused on the limitation of existing frequency ranges, identifying the 900 kHz threshold as the optimal frequency for detecting fine wire contaminants.
- Integration of Machine Learning: The software development phase saw the implementation of AI algorithms, tested across thousands of hours of real-world food production data to ensure the 3S PLUS system could accurately differentiate between products and contaminants.
- Design for the Operator: Recognizing that high-tech machines are only as good as the humans who run them, the company spent significant time refining the Human-Machine Interface (HMI). This resulted in the 10.1-inch capacitive touchscreen, designed specifically for wet, cold, or gloved industrial environments.
- North American Deployment: With the system already vetted in various international markets, the recent rollout in North America signifies a full-scale push to standardize high-sensitivity detection across the continent’s major food manufacturing hubs.
The Efficiency Imperative: Automated Performance Monitoring
A recurring theme in modern manufacturing is the move toward "lights-out" or automated verification. The M50 R-Series supports this shift through its INFINITY Electronic Test System.
Traditionally, routine performance testing of metal detectors required operators to manually pass test pieces through the line at set intervals to verify that the sensors were working correctly. This is not only time-consuming but also creates potential safety risks as operators move around moving machinery. The INFINITY system automates this process entirely. By conducting these tests without operator intervention, the system can perform verification routines up to three times faster than manual methods. This ensures that the facility is always in compliance with HACCP (Hazard Analysis and Critical Control Points) and GFSI (Global Food Safety Initiative) standards without sacrificing production speed.
Official Perspectives and Industry Implications
The introduction of the M50 R-Series comes at a time when the food industry is facing unprecedented pressure from regulatory bodies like the FDA and USDA, as well as the ever-present threat of brand damage due to recalls.
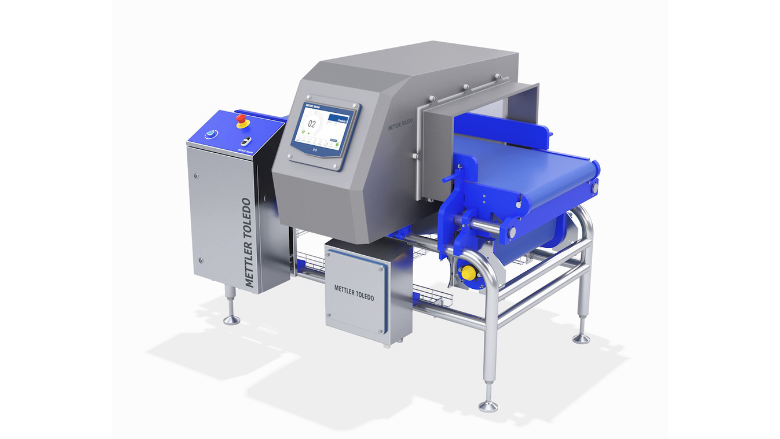
Industry experts have noted that the "connected factory" is no longer a luxury but a necessity. The M50 R-Series aligns with this by offering robust data connectivity. With embedded Wi-Fi and QR code functionality, technicians can access real-time diagnostic information via mobile devices, effectively reducing the time spent troubleshooting during a stoppage.
Furthermore, the implementation of RFID for access control solves a long-standing security issue: accountability. By requiring specific user logins for system adjustments, the M50 R-Series creates a clear audit trail. This is critical for internal compliance departments that need to know exactly who changed a sensitivity threshold or modified a product recipe, ensuring that tampering or accidental errors are quickly traced and corrected.
Supporting Data and Technical Specifications
The system’s architecture is designed for the modern "Industry 4.0" environment. Key technical features that distinguish the series include:
- Capacitive Touchscreen: A 10.1-inch interface that remains responsive even in the presence of water or when operators are wearing heavy-duty protective gloves, ensuring the machine doesn’t become a bottleneck during shift changes.
- Protocol Compatibility: Through support for OPC-UA and EtherNet/IP, the M50 R-Series can "talk" to existing plant-wide data systems, making it easier for large-scale manufacturers to centralize their quality control data.
- ProdX Integration: The detectors integrate seamlessly with Mettler Toledo’s ProdX data management software. This allows for centralized monitoring of all inspection devices, providing a bird’s-eye view of product safety across an entire manufacturing site.
- Condition Monitoring: The system tracks its own "health," providing preemptive alerts before a failure occurs. This predictive maintenance approach is essential for preventing the kind of catastrophic line failures that lead to unplanned downtime.
Implications for the Future of Food Safety
The launch of the M50 R-Series is more than just a hardware update; it is an indicator of the direction in which the food safety industry is moving. We are seeing a shift away from reactive, manual inspection methods toward proactive, data-driven systems.
Enhancing Traceability
In the event of a product recall, traceability is the manufacturer’s greatest asset. By logging every inspection event, every test result, and every user interaction, the M50 R-Series provides a detailed digital "birth certificate" for every product that passes through the line. This level of granularity is invaluable during audits and essential for rapid, accurate root-cause analysis.
Empowering the Workforce
By simplifying the user experience and automating repetitive tasks, the M50 R-Series allows human workers to focus on higher-level decision-making. Instead of manually testing metal detectors, a quality technician can focus on analyzing the data trends produced by the system to identify potential issues before they manifest as contaminated products.
Reducing Environmental and Economic Waste
Perhaps the most understated benefit of the M50 R-Series is its role in sustainability. By reducing false rejects, the system prevents thousands of pounds of perfectly safe food from being diverted to landfills or reworked. This directly supports the corporate sustainability goals of modern food companies, which are increasingly held accountable for their waste footprints.
Conclusion
The Mettler Toledo M50 R-Series AdvancedLine represents a sophisticated fusion of physical detection power and digital intelligence. For North American food manufacturers, the series offers a comprehensive solution to the challenges of modern production: the need for extreme sensitivity, the requirement for digital traceability, and the mandate for operational efficiency.
As the industry continues to evolve, the ability to integrate advanced hardware with software-driven data management will define the leaders in the field. With the M50 R-Series, Mettler Toledo has provided a blueprint for what the next generation of food safety inspection looks like—a system that is not only highly sensitive but also smart, connected, and fundamentally designed to keep the food supply chain safer than ever before.
As food manufacturers evaluate their capital expenditure for the coming years, the M50 R-Series stands out as an investment in both brand integrity and operational longevity. Whether processing meat, bakery items, or packaged snacks, the ability to detect the smallest of contaminants with the highest level of reliability is the bedrock of consumer trust. In that regard, the M50 R-Series is poised to become a staple of the modern, safety-conscious food production facility.